Bodor Laser for Sale vs. a Used Fiber Laser: A Quality Inspector’s Guide to Gantry Cutting, Copper, and Carbon Fiber
Posted on 2026-09-23 by Elise Marceau
-
What I’m comparing—and what I’m not
-
Dimension 1: Gantry fiber laser vs. open-bed stability
-
Dimension 2: Fiber laser copper—power isn’t the only spec
-
Dimension 3: Can a laser cutter cut carbon fiber?
-
Dimension 4: Spec verification, service, and hidden cost
-
When I’d choose A, and when I’d choose B
-
Bottom line
I’m a quality and brand compliance manager at a metal fabrication company. I review every machine spec and first-article cut before it reaches production—roughly 60 specs and 200 cut samples a year. In 2024, I rejected 18% of first deliveries because dimensions or edge quality missed spec. Not because the vendors were lazy. Because specs sheets don’t cut metal.
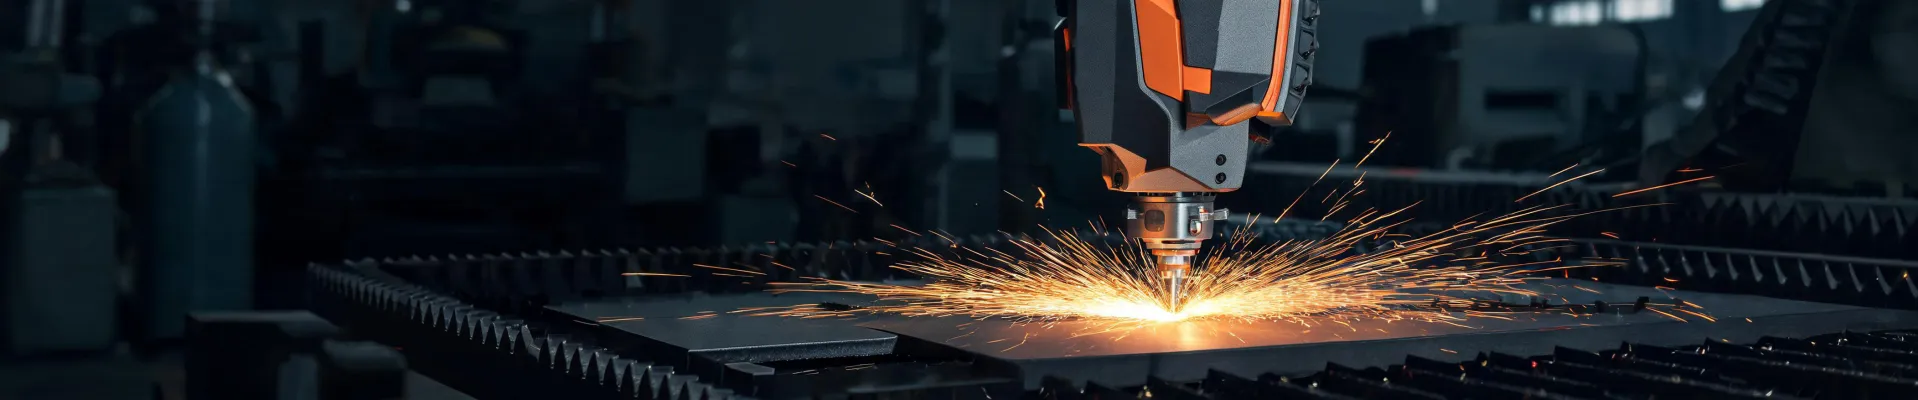
If you’re looking at a bodor laser for sale, you’re probably comparing it with something: a used fiber laser, a cheaper import, or a no-name machine advertised as “same factory.” I’m going to compare two buying paths I’ve actually audited: A) a documented Bodor gantry fiber laser from a traceable OEM or authorized channel, and B) a used or rebranded fiber laser with vague history. The criteria: frame and gantry design, copper cutting, carbon fiber reality, and service/spec verification.
Per FTC advertising guidelines (ftc.gov), claims must be truthful, not misleading, and substantiated with evidence. That applies to “cuts copper” and “cuts carbon fiber” claims just as much as to any consumer ad.
What I’m comparing—and what I’m not
I’m not saying every used machine is bad. I’ve seen used equipment outperform new equipment when the previous owner kept records. But here’s the thing: with a capital laser cutter, the risk isn’t just the machine. It’s the unknowns—laser source hours, chiller condition, calibration history, and whether the parameters were ever validated on real production parts.
So the comparison is simple. A is a China Bodor laser cutting machine bought through a channel that can show test reports, laser source serial numbers, and first-article samples. B is a machine where the seller says “it works great” and has maybe one photo of it cutting thin mild steel.
Dimension 1: Gantry fiber laser vs. open-bed stability
The first place I see difference is the frame. A gantry fiber laser carries the cutting head on a rigid bridge that moves over a fixed bed. That design usually gives you better vibration control on thick plate and reflective material. An open-bed or lighter-frame machine can be fine for thin sheet, but it gets sketchy when you push it hard for eight hours.
I ran a side-by-side audit last year: same 6 kW power class, same 4 mm copper, same nitrogen assist gas. The gantry machine held edge taper within our tolerance for the full shift. The lighter used machine started drifting after about four hours. Not a catastrophic failure. But our tolerance didn’t care about excuses.
Honestly, I’m not sure why some gantry machines hold tolerance after eight hours while others drift. My best guess is frame mass and thermal compensation. Either way, if you’re cutting copper or thick stainless daily, gantry design is not marketing fluff. It’s a quality control feature.
My verdict: For copper above 3 mm and multi-shift production, A wins. For thin-gauge mild steel and one-shift work, B can be workable—if you inspect first article and every four hours.
Dimension 2: Fiber laser copper—power isn’t the only spec
Copper is reflective, thermally conductive, and annoying. A fiber laser can cut copper, but not every fiber laser cuts copper well. The wavelength helps, but the real difference is in the setup: beam quality, nozzle condition, focus position, pierce strategy, and assist gas pressure.
Everything I’d read about fiber laser copper said more kW equals better cuts. In practice, on our 4 mm copper trial, a well-tuned 6 kW machine beat a poorly tuned 12 kW machine on dross and edge squareness. The 12 kW had more power. It didn’t have the right parameters.
When I compare A and B, I ask for the same sample set: 3 mm, 5 mm, and 8 mm copper, cut with production parameters, not demo parameters. Then I measure dross, taper, and heat-affected zone. If the seller can’t provide copper samples, the claim is unsubstantiated. That’s not a technicality. It’s how you avoid a $40,000 mistake that only shows up after the machine is on your floor.
My verdict: A documented Bodor fiber laser with copper parameter files and sample cuts is a known risk. A used machine with a “copper-ready” sticker is an unknown risk. If copper is more than 20% of your workload, pay for the sample test.
Dimension 3: Can a laser cutter cut carbon fiber?
Yes. But the useful answer is: sometimes, and not like metal. A fiber laser can cut thin carbon fiber sheets, but carbon fiber isn’t steel. It’s resin and carbon. The laser creates a heat-affected zone, potential fraying, charring, and fumes that need extraction. If you’re asking can a laser cutter cut carbon fiber, the next question should be: at what edge quality, and with what safety controls?
I’ve rejected carbon fiber parts that looked fine on the top surface but had a charred, delaminated edge. The vendor said the machine could cut it. It could. It just couldn’t cut it to our spec.
In the A vs. B comparison, A has an advantage if the machine is documented, enclosed, and set up with proper fume extraction and parameter control. B—a used machine with unknown maintenance—can cut carbon fiber, but you’re rolling the dice on consistency and safety. And if carbon fiber is a major part of your production, don’t default to a fiber laser just because it’s a laser. Waterjet or abrasive cutting may be the better process.
My verdict: For occasional carbon fiber, A with extraction and testing can work. For daily carbon fiber, neither A nor B is automatically the right tool. Match the process to the material.
Dimension 4: Spec verification, service, and hidden cost
The most frustrating part of evaluating laser cutters: the spec sheets look identical until you cut real material. You’d think a 6 kW is a 6 kW, but edge taper tells a different story. That’s why I treat the purchase as a compliance audit, not a shopping cart.
With A, I can ask for:
- Laser source serial number and original test report
- CE or FDA laser safety documentation, depending on destination
- Enclosure interlocks and class rating
- First-article samples on copper, stainless, aluminum, and carbon fiber
- Training records and parameter backup
- Itemized quote: chiller, compressor, extraction, installation, freight
With B, you can still ask. But if the answer is “I don’t have that,” you have to price in the risk. A replacement fiber source, a new chiller, or a week of downtime can erase the savings fast. Look, I’m not saying used machines are always bad. I’m saying they’re riskier unless you can verify the history.
My verdict: A documented Bodor laser for sale is not the cheapest path. It’s the most verifiable path. For a shop that runs production deadlines, verifiability has value.
When I’d choose A, and when I’d choose B
Choose A—a documented Bodor gantry fiber laser—if you cut copper over 3 mm, run multiple shifts, need traceable service, or mix in occasional carbon fiber with proper extraction. It’s also the safer choice if you don’t have an in-house laser maintenance tech.
Choose B—a used or entry-level fiber laser—if you cut thin mild steel, have a strong maintenance team, and can inspect the machine under power before buying. It can be a smart buy for a job shop with simple work. Just don’t expect the same support or traceability.
If you’re stuck between the two, run the same test on both: a 4 mm copper sample, a 6 mm stainless sample, and a thin carbon fiber sample. Measure the edge. Check the fumes. Ask for the maintenance log. The machine that passes is the one you buy.
Bottom line
A Bodor laser for sale through a documented channel isn’t automatically right for every shop. But when I compare it with a used machine of unknown history, the difference isn’t just price. It’s whether you can prove the machine will hold your spec after 1,000 cuts. That’s the standard I use. It’s the standard I’d want if I were standing on the production floor at 2 a.m.
Not glamorous. Just how quality works.
Elise Marceau
Elise Marceau is an LED display and digital-signage systems analyst covering LED video walls, modular screens, transparent LED, control processors, and indoor or outdoor signage. She applies IEC 62368-1 safety principles while comparing pixel pitch, luminance, contrast, refresh rate, colour uniformity, viewing angle, ingress protection, power density, module serviceability, and signal redundancy. Her specification guides help integrators, venue operators, retailers, and procurement teams align viewing distance, ambient light, content format, installation access, electrical load, and lifecycle support.